

Industrial Concrete Floor Coatings for Tough Needs
When tackling tough industrial needs, opt for industrial concrete floor coatings. They offer durability and reliability against heavy loads and harsh conditions. Benefits include cost-effectiveness, protection from spills, and customization options. Epoxy, polyurethane, polyurea, and MMA coatings cater to different requirements. Consider factors like foot traffic and existing issues before coating. Follow a meticulous application process – clean, repair, prime, apply, and cure. Regular maintenance enhances longevity, ensuring resistance and integrity. For more insights into types of coatings, factors to consider, application tips, and maintenance advice, explore further.
Benefits of Industrial Concrete Floor Coatings
When outfitting industrial spaces, we rely on concrete floor coatings for their durability and protective qualities. Industrial concrete floor coatings offer numerous benefits that are essential for maintaining a safe and efficient work environment. One significant advantage is the cost-effectiveness of industrial epoxy floor coatings. While initial installation costs may be higher compared to other flooring options, the long-term savings in maintenance and repair make them a wise investment for industrial settings. Additionally, these coatings provide exceptional protection against heavy loads and chemical spills, ensuring the longevity of the floor surface.
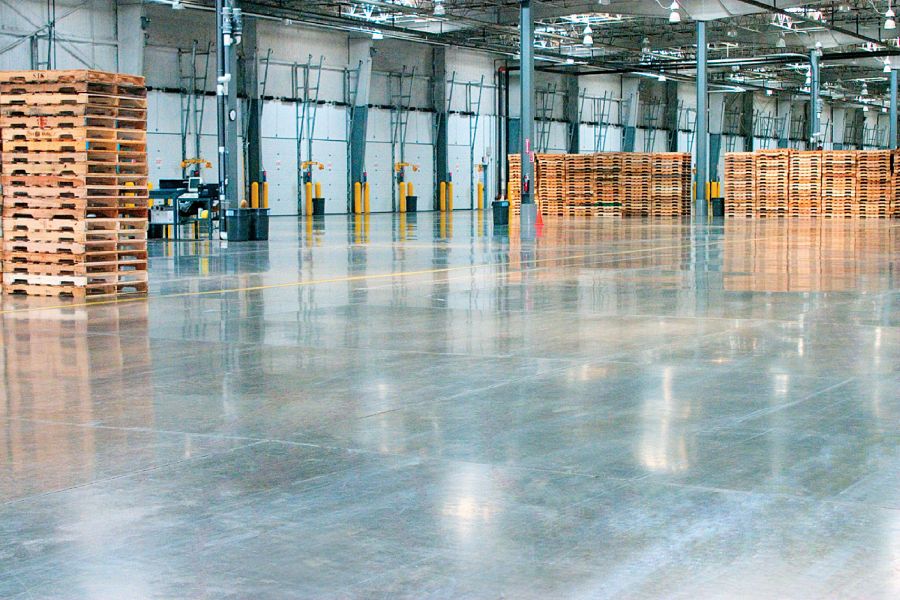
Warehouse floor coating options are crucial considerations when selecting the most suitable coating for industrial spaces. The diverse range of coatings available allows us to customize solutions based on the specific needs of the facility. Whether the priority is slip resistance, abrasion resistance, or ease of maintenance, there’s a floor coating option to meet those requirements effectively.
Inevitably, industrial spaces may experience wear and tear over time, leading to the need for industrial concrete floor repair. By utilizing high-quality coatings, we can address any damage promptly, extending the lifespan of the flooring and minimizing disruptions to operations. Investing in regular maintenance and repairs can prevent more extensive damage in the future, saving both time and money in the long run.
Types of Industrial Floor Coatings
As we explore industrial floor coating options, it becomes evident that understanding the various types available is key to meeting specific performance requirements. Industrial floor coatings come in different formulations to address diverse needs. Epoxy coatings are popular for their durability and chemical resistance, making them suitable for areas exposed to harsh substances. These coatings are also customizable in terms of colors and patterns, adding aesthetics to their functionality.
Polyurethane coatings offer excellent abrasion and impact resistance, making them ideal for environments with heavy machinery or high traffic. They’re also known for their UV stability, preventing discoloration and degradation when exposed to sunlight. For areas requiring anti-slip properties, polyurea coatings provide a textured surface that enhances safety without compromising on durability.
In facilities where fast installation is crucial, methyl methacrylate (MMA) coatings are a great choice due to their quick cure time, allowing for minimal downtime. These coatings are also resistant to chemicals and can withstand temperature extremes, making them versatile for various industrial settings.
Each type of industrial floor coating has its unique characteristics, and selecting the right one depends on the specific requirements of the facility. By evaluating factors such as durability, chemical resistance, aesthetics, and installation time, businesses can choose the most suitable coating to enhance the longevity and performance of their industrial floors.
Factors to Consider Before Coating
Considering the specific requirements of your industrial space is crucial before applying any concrete floor coating. Factors such as the type of industry, the level of foot and vehicle traffic, exposure to chemicals or heavy machinery, and the desired appearance all play a significant role in determining the most suitable coating for your facility. Understanding these key elements will help you choose a coating that will withstand the demands of your environment and provide long-lasting protection.
Another essential factor to consider is the condition of the existing concrete substrate. Any cracks, spalling, or moisture issues should be addressed before applying a coating to ensure proper adhesion and performance. Conducting a thorough inspection and preparing the surface accordingly will help avoid future maintenance problems and costly repairs.
Moreover, budget and timeline constraints are vital considerations before coating your industrial floor. Different coatings have varying costs and curing times, so it’s essential to select an option that aligns with your financial resources and operational schedule. Additionally, considering the potential impact of downtime during the coating application process is crucial for minimizing disruptions to your business operations.
Application Process for Concrete Coatings
Before proceeding with the application process for concrete coatings, it’s important to address any existing issues with the concrete substrate to ensure optimal adhesion and performance. The first step is to thoroughly clean the concrete surface by removing any dirt, grease, or contaminants. This can be done through pressure washing or chemical cleaning. Any cracks, spalls, or imperfections in the concrete should be repaired using suitable patching materials to create a smooth and level surface.
Next, the concrete should be profiled to promote adhesion. This can be achieved through methods such as shot blasting or diamond grinding, which create a rough texture for the coating to grip onto. Once the surface preparation is complete, a primer may be applied to enhance adhesion and ensure a strong bond between the concrete and the coating.
When it comes to applying the concrete coating, follow the manufacturer’s instructions regarding mixing ratios, application methods, and curing times. Typically, a roller or brush is used to apply the coating evenly across the surface. Multiple coats may be necessary to achieve the desired thickness and performance characteristics.
After the coating has been applied, it’s essential to allow sufficient time for curing before subjecting it to foot traffic or heavy loads. Proper curing will help ensure the longevity and durability of the concrete coating, providing a high-performance solution for your industrial space.
Maintenance and Longevity Tips
To maintain the durability and longevity of your concrete floor coating, regularly inspect for any signs of wear or damage. Check for areas where the coating may be peeling, cracking, or showing excessive wear due to heavy traffic or chemical exposure. Addressing these issues promptly can prevent further damage and prolong the life of your floor coating.
In addition to inspections, it’s essential to clean your concrete floor regularly to remove debris, dirt, and potentially corrosive substances. Use a gentle cleanser or a manufacturer-recommended cleaning solution to avoid damaging the coating. Avoid harsh chemicals that can deteriorate the coating prematurely.
Consider applying a fresh topcoat or sealer every few years to enhance the protective properties of your industrial concrete floor coating. This maintenance step can help maintain the integrity of the coating and increase its resistance to abrasion, chemicals, and UV exposure.
If you notice any significant damage or wear during your inspections, consider contacting a professional to assess the situation. They can guide the best course of action, whether it’s a localized repair or recoating the entire floor surface.
Key Takeaways
- Industrial epoxy coatings provide cost-effective durability and chemical resistance.
- Polyurethane coatings offer abrasion and impact resistance for tough industrial needs.
- Polyurea coatings are ideal for anti-slip properties in high-traffic areas.
- Fast installation with Methyl methacrylate (MMA) coatings for minimal downtime.
- Choose the right coating based on industry, traffic levels, and budget for longevity.
Benefits of Industrial Concrete Floor Coatings – Additional Insights
Enhanced Chemical and Spill Resistance
Improved Slip Resistance
Aesthetic Enhancement
Noise and Vibration Reduction
Long-Term Cost Savings
Comparison Table: Industrial Concrete Floor Coatings
Maintenance Tips for Industrial Concrete Floor Coatings
- Regular Cleaning – Sweep or mop daily to remove debris and prevent abrasion.
- Prompt Spill Cleanup – Address chemical or oil spills immediately to avoid staining or surface damage.
- Periodic Inspections – Look for peeling, cracking, or worn areas and address them before they worsen.
- Topcoat or Recoating – Refresh the protective layer every few years to maintain chemical and abrasion resistance.
- Avoid Harsh Abrasives – Use gentle cleaners recommended by the coating manufacturer.
Professional vs. DIY Concrete Coating
Specialty Applications of Industrial Concrete Coatings
- Loading Docks & High-Traffic Areas – Resistant to wear from forklifts, pallets, and heavy foot traffic.
- Chemical Storage Zones – Provides protection against corrosive spills and harsh substances.
- Cold Storage & Freezers – Certain coatings resist moisture and thermal cycling.
- Outdoor Industrial Yards – UV and weather-resistant coatings extend surface life under sun, rain, and temperature changes.